Inside a CNC Milling Machine Factory: Precision Manufacturing Unveiled
2026-07-20
Step inside a world where raw metal transforms into precision-engineered components with microscopic accuracy. In the heart of modern manufacturing, CNC milling machines orchestrate a symphony of cutting tools and computer-controlled movements, turning digital designs into tangible reality. This journey into the factory floor reveals the seamless integration of advanced technology and human expertise that defines WINNRUI CNC. From the initial CAD model to the final finished part, every step is a testament to innovation. But what truly sets this process apart? Join us as we unveil the hidden intricacies of precision manufacturing and discover why WINNRUI CNC is at the forefront of the industry.
Spindles Spinning: The Heartbeat of the Machine
In any spinning frame, the spindle is where raw fiber transforms into thread. It’s a small, whirring component, often overlooked, yet it sets the rhythm for the entire production floor. Each rotation pulls, twists, and winds the yarn with a precision that borders on hypnotic. When dozens or hundreds of them spin together, they create a low, constant hum—the machine’s pulse. You can feel it through the floorboards, a steady vibration that tells you things are running as they should.
There’s an art to keeping this heartbeat steady. Spindle speed, tension, and the condition of the ring and traveler all play their part. Too slow, and the yarn lacks twist; too fast, and breakages pile up. A skilled operator learns to read the sound, the slight changes in pitch that signal wear or misalignment. They listen with more than just ears—fingertips resting on the frame catch the subtle tremors. It’s this intimate dialogue with the machine that separates a mere worker from a true spinner.
Over centuries, spindles have evolved from simple hand-held sticks to today’s high-speed, air-bearing designs. Yet the principle remains unchanged: spin to bind, spin to strengthen. Even in an age of automation, the spindle’s heartbeat stays central to textile creation—a timeless link between the craftsman’s touch and the hum of industry.
G-Code and Toolpaths: The Invisible Sculptor
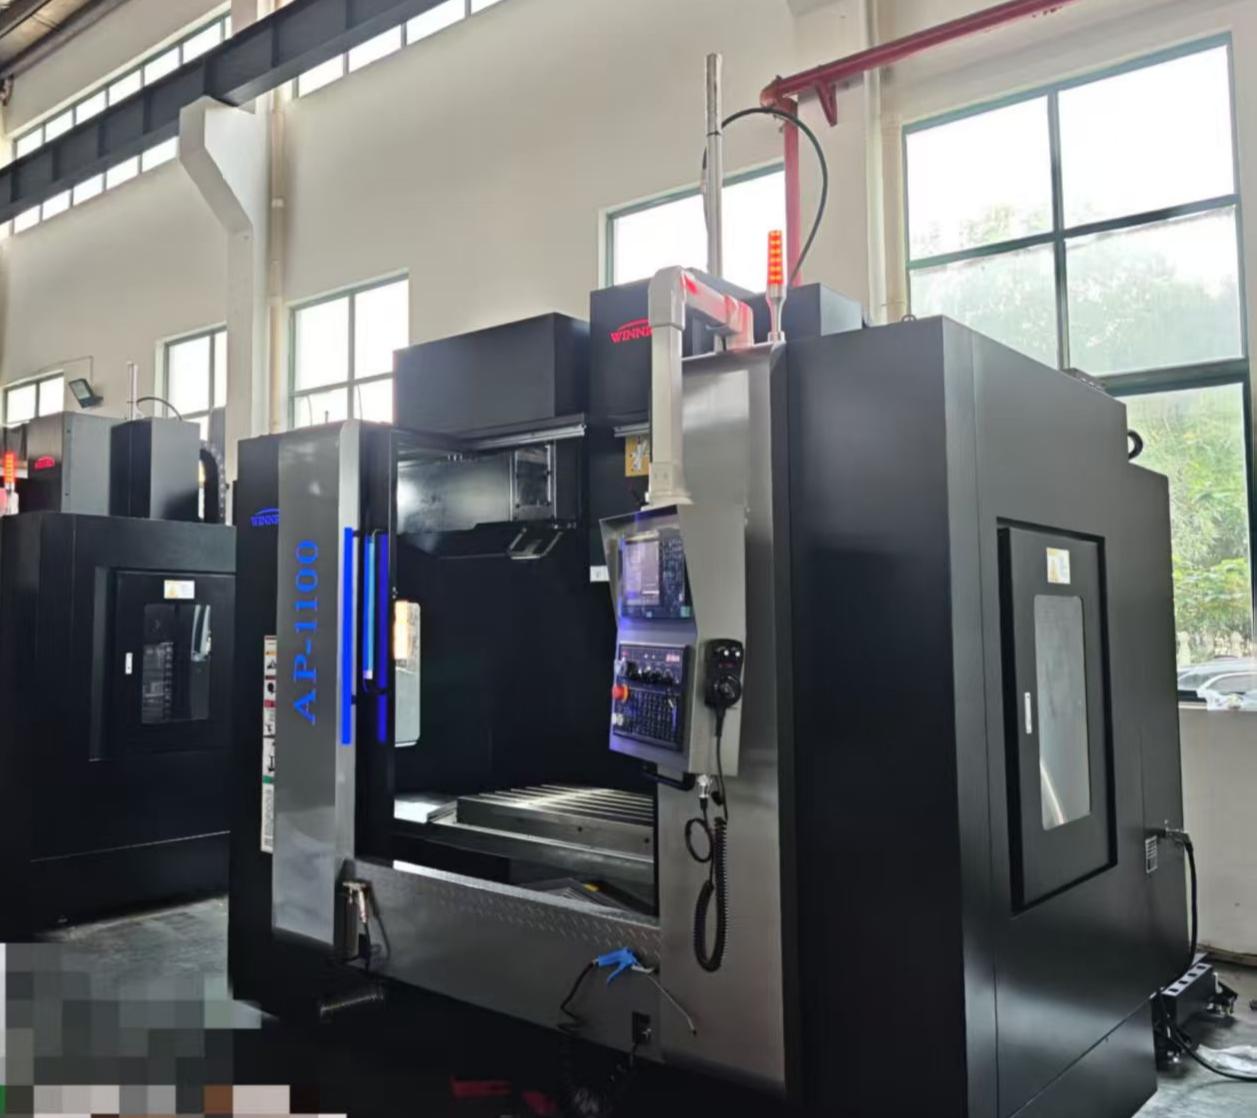
At its heart, every CNC creation begins with a silent conversation between machine and material, spoken in a language most never see—G-code. This string of coordinates and commands might look like cryptic poetry, but it’s the precise script that drives the tool through space, carving air into art. A toolpath isn’t just a line on a screen; it’s the choreography of the cutter, determining not only the final shape but the very texture of the surface. Choose a parallel finish pass, and you get a subtle, linear rhythm. Opt for a spiral morph, and the tool flows like water around contours, leaving behind a whisper of its journey. Every scallop height, every stepover, is a deliberate choice that sculpts light and shadow into the part.
Yet the invisible hand of toolpaths reaches deeper than aesthetics. It governs efficiency, tool life, and the very possibility of reaching into impossible undercuts. Think of a 5-axis swarf cut sliding along a ruled surface, or a trochoidal peel that nibbles away material with constant engagement, never biting off more than it can chew. These strategies are born from physics as much as geometry, balancing cutting forces to avoid chatter, managing heat to prevent work hardening, and keeping the tool safely tucked in tight corners. Even the seemingly mundane linking moves—those rapid traverses above the part—are carefully threaded by a skilled programmer to avoid collisions, like threading a needle in three dimensions at 60 miles per hour.
What’s often overlooked is how deeply personal a toolpath can become. Two machinists given the same CAD model will likely weave entirely different paths: one might favor a constant scallop strategy for a silky finish, while another leans on a pencil trace to sharpen creases and edges that catch the thumb. The software offers endless knobs to turn—tolerance bands that whisper “follow the surface within a micron,” or smoothing that blends tangency breaks into fluid arcs. It’s a blend of engineering and art, where experience tunes the algorithm, and the invisible sculptor leaves its fingerprint in every curved reflection.
Coolant, Chips, and Chatter: Managing the Mess
Every machinist knows the trio of troublemakers: coolant spraying where it shouldn’t, chips piling up like metallic confetti, and chatter that rattles both the workpiece and your nerves. Managing this mess isn’t just about cleanliness—it’s about precision. A well-directed coolant stream not only cools the cut but also flushes chips away from the tool, preventing re-cutting and tool wear. But when the pressure is off or the nozzle misfires, chips cling to the tool, and suddenly you’re fighting a sticky, abrasive cloud. The key is tuning the system so coolant, chips, and tool work in concert rather than collision.
Chatter often signals a deeper imbalance—maybe the tool overhang is too long or the spindle speed is slightly off its sweet spot. Rather than chasing it with endless parameter tweaks, try shifting your perspective: treat the setup as an interconnected system. A chip evacuation issue can mimic chatter, and a coolant nozzle straying out of position can leave chips where they don’t belong. Sometimes the fix is as simple as repositioning a nozzle or swapping to a through-tool coolant delivery, turning a messy, noisy cut into a smooth, predictable one.
Measuring to Microns: The Quality Gatekeepers
Precision isn't just a goal in modern manufacturing—it's the baseline expectation. When tolerances slip into the micron range, the margin for error vanishes. Components that once relied on human inspection now pass through a gauntlet of automated measurement systems, each one tuned to catch deviations invisible to the naked eye. These aren't simple calipers or micrometers; we're talking laser interferometry, white-light scanning, and coordinate measuring machines that map surfaces with sub-micron repeatability. They don't just verify parts—they define what's acceptable in an environment where a single stray particle can ruin a batch.
The real shift isn't the hardware itself, but how data flows from these instruments. A measurement taken at 3 a.m. in a factory in Stuttgart can trigger an alert on a quality engineer's phone in Chicago before the shift even changes. The gatekeepers have become predictive, using statistical process control that learns from every cycle. If a tool begins to wear, the system flags it before a single out-of-spec part is produced. This is quality assurance that doesn't just react—it anticipates, reshaping the relationship between production speed and final inspection.
Yet for all the automation, the human element hasn't disappeared—it's simply moved upstream. Someone still has to understand uncertainty budgets, interpret thermal compensation graphs, and decide when a measurement strategy needs rethinking. The gatekeepers of today blend metrology expertise with data science, troubleshooting sensor drift as deftly as they coach line operators on handling delicate surfaces. It's a discipline that demands equal parts patience and skepticism, because when you're chasing microns, the biggest threats often hide in plain sight: a draft from an open bay door, a floor vibration from a passing forklift, or a fixture that's been assembled slightly off-square for months. The best quality gatekeepers know that the instruments are only as reliable as the attention paid to their environment.
Automated Cells: Where Robots Load and Unload
Picture a manufacturing floor where machines never pause for breaks. Automated cells turn this vision into reality by using robots to handle the repetitive chore of loading raw parts and unloading finished pieces. These self-contained workstations orchestrate a seamless dance between a robot arm, a CNC machine, and a conveyor. The robot picks a blank from a tray, places it precisely in the chuck, and retrieves the completed component once machining ends. No human intervention is needed for hours, freeing skilled operators to focus on more complex tasks. This not only slashes idle time but also eliminates the ergonomic strain of manual material handling.
The true strength of an automated cell lies in its adaptability. Unlike rigid hard automation from decades past, modern cells can switch between product variants with little more than a program change. For example, a single robot may load a casting for the morning shift, then handle a delicate electronic housing in the afternoon, all while a vision system confirms part orientation and quality. Quick-change grippers and automatic jaw adjustment on the chuck allow the switchover to happen in minutes. This flexibility makes automated cells indispensable for high-mix, low-volume production environments where every batch demands a different touch.
Yet, the technology goes beyond mere parts movement. Today’s cells integrate in-process inspection, deburring, and even basic assembly. A robot might unload a milled part, present it to a camera for dimension checks, and then place it directly into a cleaning station before setting it on an outgoing pallet. By combining operations, the cell shrinks lead times and reduces work-in-progress inventory. Data streams from sensors feed back into the factory network, allowing predictive maintenance and real-time monitoring. Ultimately, automated cells blur the line between material handling and full-scale manufacturing, proving that loading and unloading is just the beginning of what these robots can accomplish.
From Apprentice to Artisan: The Human Element
Craftsmanship isn't merely a checklist of skills acquired; it's a gradual, often messy journey of internalizing trade secrets through countless failures. The human element is the quiet whisper of intuition that guides a hand to correct a subtle error before it becomes a flaw—something no manual can fully impart.
When you transition from apprentice to artisan, you stop merely replicating techniques and start embodying them. The human element reveals itself in the unique signature each craftsperson leaves behind: a slight variation in texture, an unexpected solution to a unique problem, or the way they adapt ancient methods to modern materials.
Ultimately, the human element is the capacity for empathy and storytelling. An artisan doesn't just produce an object; they infuse it with meaning drawn from personal experience and cultural memory. This is what elevates utilitarian work into something that resonates across generations—something algorithms and automation can never replicate.
FAQ
A CNC milling machine uses computer-controlled movements to cut and shape materials with extreme precision, unlike manual milling where an operator physically guides the tool. The automated process reduces human error and allows for complex, repeatable designs that would be nearly impossible by hand.
Most factories are organized into distinct zones: raw material storage, the main machining area with rows of CNC mills, a quality inspection section equipped with CMMs and laser scanners, and a finishing area for deburring and cleaning. Overhead cranes and automated guided vehicles often move parts between stations.
Aluminum, steel, brass, and various plastics dominate because of their machinability and wide industrial use. Aerospace often demands titanium and exotic alloys, while electronics manufacturers favor non-conductive materials. The choice depends on the final product’s strength, weight, and thermal requirements.
It relies on a combination of rigid machine construction, high-quality ball screws and linear guides, closed-loop feedback from encoders, and strict temperature control. Regular calibration with laser interferometers confirms positioning accuracy, while in-process probing checks dimensions without unclamping the part.
Operators aren’t just button-pushers; they set up workholding, verify tool offsets, inspect the first part off the machine, and listen for abnormal sounds that indicate tool wear or programming errors. Their experience is crucial for troubleshooting and optimizing feeds and speeds.
CAM software takes a CAD model and translates it into G-code—a language of coordinates and commands. It plans the toolpaths step by step: roughing cuts to remove bulk material, then finishing passes for tight tolerances. Post-processors tailor the code to the specific CNC machine’s controller.
Beyond coordinate measuring machines, you’ll see surface roughness testers, hardness testers, and sometimes vibration analysis tools. Parts may be marked with QR codes for traceability, linking each component to its inspection report and machine data. Random sampling and full batch checks depend on the industry's criticality.
Conclusion
Walking through a CNC milling factory, the hum of spindles immediately sets the rhythm—a constant, high-pitched whir that underscores the transformation of raw metal into precision parts. These spindles, spinning at dizzying speeds, are the literal heartbeat of the machines, but the true artistry lies in the invisible code guiding them. G-codes, meticulously crafted by skilled programmers, map out every toolpath, choreographing a dance of cutters that removes material in layers so fine they’re measured in microns. The process is anything but clean; a blizzard of chips erupts as coolant jets flood the cutting zone, suppressing heat and clearing debris while operators listen intently for chatter—that telltale vibration that signals trouble. Managing this chaos is a science in itself, balancing fluid chemistry and chip evacuation to keep the operation both stable and accurate.
Once milling is complete, parts pass through a gauntlet of measurement tools where tolerances are enforced down to the micron. Optical comparators and coordinate measuring machines stand as the final judges, rejecting anything that strays from the digital blueprint. In many modern shops, this inspection is integrated into automated cells where robotic arms tirelessly load and unload workpieces, merging speed with consistency. Yet, technology alone doesn’t define the floor. The real pulse comes from the people—apprentices learning to read the sound of a cut, seasoned machinists who can hear a dull insert before a sensor catches it, and programmers who balance efficiency with tool life. It’s a world where hands-on intuition and digital precision merge, transforming raw stock into components that power industries.
Contact Us
Contact Person: Tim
Email: [email protected]
Tel/WhatsApp: +86 15522553731
Website: https://www.winnrui-cnc.com/