Megasonic Cleaning System Vendor Selection Guide for Precision Manufacturing
2026-10-08
Megasonic cleaning may be invisible in the final product, but in precision manufacturing it's often the difference between a passing lot and a quiet yield killer. If you're evaluating vendors, this guide was written for you—not to list features, but to surface the questions that expose whether a system can hold up under real process conditions. From transducer design to particle removal repeatability, we'll break down what to weigh before you sign. And when it comes to proven megasonic performance, Siansonic is one name worth putting on your shortlist early.
Before You Send RFQs, Define the Contaminant You're Actually Fighting
Most teams rush into the RFQ process with a vague sense of "we need better filtration" but no clear definition of the actual contaminant. Is it airborne dust from a specific process? A chemical byproduct that only appears under certain temperatures? Oil mist that coalesces differently depending on humidity? Without pinning down the exact particle size, chemical composition, and concentration range, every quote you receive is based on guesswork — and every filter tested becomes a shot in the dark.
A practical approach is to spend a day on the floor with a simple sampling kit before drafting a single RFQ. Collect residue from different shifts, note when the problem spikes, and run basic gravimetric or microscopy tests. You might discover that what was called "fine dust" is actually a mix of 2-micron abrasive particles and sticky mold-release aerosol — a combination that demands entirely different media and drainage geometry than the generic high-efficiency panel your last supplier quoted.
That clarity changes the conversation with potential vendors. Instead of comparing identical-looking datasheets, you can ask specific questions: How does your coalescer handle intermittent surfactant loading? What's the pressure-drop curve at 95% relative humidity for this particle distribution? Suppliers who engage with those details are the ones worth shortlisting. The ones who still send back a one-page quote with no technical questions? You already know they never understood the problem.
Transducer Frequency Specs Look Similar, but Cavitation Behavior Is Not
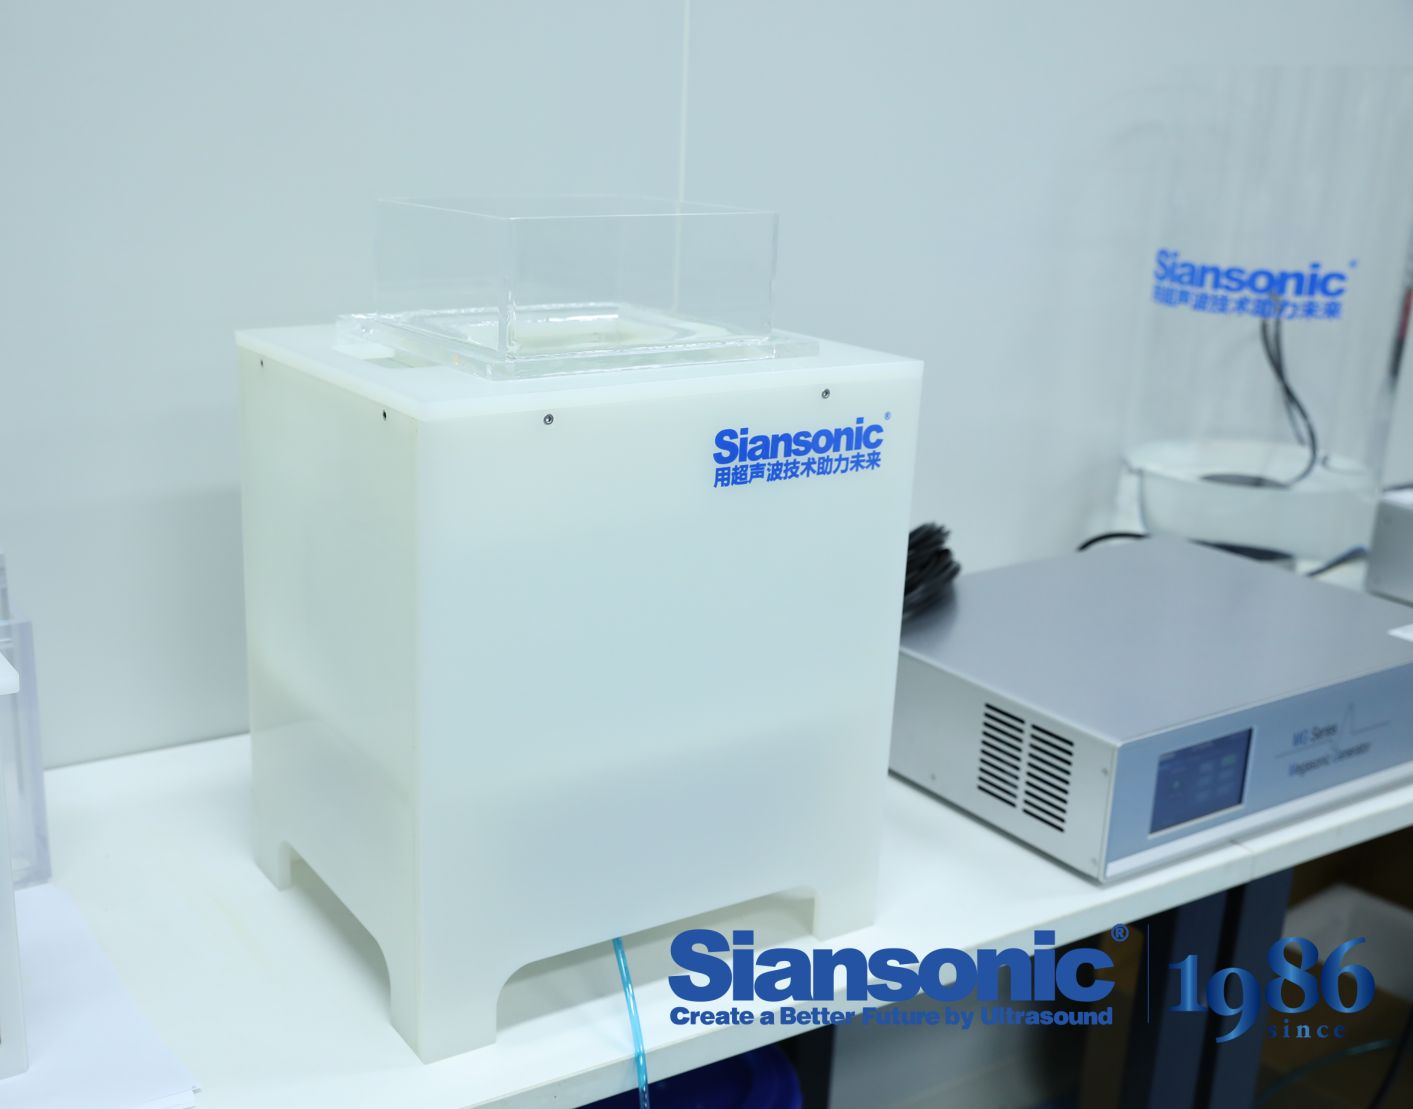
Two ultrasonic transducers can share the same frequency rating on paper—say, 40 kHz—yet behave very differently when they start driving cavitation in a liquid. The numerical frequency only tells part of the story. Actual cavitation intensity depends on factors like the transducer's amplitude, the shape and material of its radiating face, and how cleanly it couples energy into the fluid. A well-designed 40 kHz transducer with high displacement and a tuned horn can generate dense, energetic cavitation bubbles that aggressively scrub surfaces, while another 40 kHz unit with lower amplitude or a mismatched horn may produce just a faint mist of fine bubbles that barely lifts contaminants.
This gap often shows up in real-world cleaning or processing tasks. For example, a precision-cleaning line for delicate electronic components might use a 40 kHz transducer that has been deliberately damped and shaped to produce a soft, uniform cavitation field—enough to remove flux residues without damaging wire bonds. Switch to a different 40 kHz transducer, perhaps one with a thicker piezoelectric stack and a solid metal horn, and the same tank suddenly becomes harsh enough to pit soft metals or erode coatings. The frequency spec looks identical on the datasheet, but the cavitation behavior reveals a completely different energy delivery profile.
The reason lies in how the transducer converts electrical drive into mechanical motion and then into pressure waves. Even at the same nominal frequency, differences in piezoelectric ceramic grade, backing material, node placement, and horn geometry shift the resonance slightly and change the distribution of anti-nodes across the radiating surface. Those subtle variations alter the threshold at which cavitation starts, the size distribution of the bubbles, and the collapse intensity. So when selecting a transducer for a process, it's risky to assume that matching the frequency number will give you the same cavitation result. Bench testing under actual liquid and load conditions is the only reliable way to compare units that look the same on paper.
The Cleaning Chemistry and Megasonic Energy Must Be Tuned as a Pair
Cleaning efficiency in semiconductor manufacturing rarely hinges on a single variable. The chemistry you choose and the megasonic energy you apply behave like two sides of the same coin. If the chemical concentration is too aggressive, it can etch delicate features before cavitation even becomes useful. If the megasonic power is too high, it may create collapse events that damage surfaces or generate unwanted particles. The real skill lies in finding the narrow window where they reinforce each other without crossing into harm.
A common mistake is treating megasonic energy as a simple amplifier for chemical action. In practice, the bubble dynamics shift as the chemistry changes. Surfactant load, pH, and dissolved gas content all influence how cavitation bubbles nucleate and collapse. Raise the power blindly and you may turn a gentle scrubbing action into a shockwave source that pits fragile films. Lower it too much and residues linger in high-aspect-ratio trenches. The pair must move together—sometimes a tweak in chemistry allows you to drop megasonic power by fifteen percent and still hit the same particle removal efficiency.
Tuning them as a pair also changes how you approach process monitoring. Instead of optimizing each parameter independently, you track a combined response: defect count after clean, film loss, and surface roughness. A shift in incoming wafer condition often requires rebalancing both knobs simultaneously. Experienced engineers keep a small matrix of chemistry-power combinations mapped for different device nodes. That way, when a new residue type appears, they already know which direction to turn the pair—not just one dial at a time.
Tank Geometry Can Undo Your Particle Removal Rate
It’s tempting to assume that a bigger tank automatically means better settling, but the shape of that volume often matters more than the total capacity. A cylindrical clarifier with a steep cone bottom may look efficient on paper, yet the narrow angle can force solids into a slow-moving boundary layer where they resuspend instead of compacting. Even a modest change in the cone slope—say from 60 degrees to 45—can shift the effective settling area enough to cut particle capture by double digits.
Inlet and outlet placement adds another layer of trouble. When the feed enters tangentially or too close to the overflow weir, short-circuiting lets a portion of the flow bypass the quiescent zone entirely. That means particles that should have dropped out in the first third of the tank end up leaving with the clarified stream. A simple baffle or a relocated dip tube can often recover more removal efficiency than a 20% increase in tank volume.
The real danger is that these geometry-driven losses are invisible in a standard total suspended solids test. You might be hitting your target on average while a persistent fraction of fine particles slips through a dead corner or an eddy behind the outlet nozzle. Mapping the actual flow path—even with a dye test—usually reveals that the tank is working against itself, not for you.
A Vendor's Cleanroom References Matter More Than Their Marketing Claims
When a cleanroom supplier hands you a glossy brochure full of ISO certifications and zero-defect promises, the most valuable page is often missing: the list of clients who will actually take your call. A vendor's existing customers have already paid the price for their mistakes, learned which corners get cut when deadlines slip, and discovered whether the cleanroom performs as specified on day 400, not just day one. Those references are the only unscripted audit you'll get, so if a vendor hesitates to share them, treat that pause as a red flag louder than any marketing slogan.
Marketing claims are engineered to survive a five-minute sales pitch; cleanroom references are forged in months of real operation. Ask a reference about the time a particle count drifted out of spec at 2 a.m., or how the vendor handled a delayed filter shipment during a production ramp-up. The answers—or the awkward silence—will tell you more about their engineering depth and service culture than a polished case study ever could. A vendor that proactively connects you with two or three customers who pushed their system to the limit, rather than a single handpicked showcase, is demonstrating confidence that marketing budgets simply cannot buy.
The cleanroom industry is full of vendors who shine in the proposal stage and fade once the validation documents are signed. References are your only real defense against that pattern. They don't just confirm that the cleanroom works; they reveal how the vendor behaves when it doesn't. In an environment where a single overlooked gasket or misconfigured pressure cascade can invalidate an entire batch, the difference between a vendor's promise and a customer's lived experience is often the difference between compliance and a costly shutdown.
Run a Controlled Damage Study Before Signing Off on the System
Most teams spend weeks validating happy-path scenarios, then sign off on a system without ever seeing how it behaves when something actually breaks. A controlled damage study flips that approach: you deliberately introduce failures while the system is still in your hands. Pull a database replica offline mid-transaction, throttle network traffic between two services to near zero, or send a burst of malformed requests to the API gateway. Watch how the system degrades, whether it isolates the fault, and how long it takes to restore a consistent state. These observations tell you far more about operational readiness than a clean test suite ever will.
The key is to treat each injected fault as a data point rather than a pass/fail checkbox. For instance, if you kill a message broker node, does the remaining cluster keep accepting writes, or do producers start timing out and dropping events? If you corrupt a small fraction of records in a read replica, do users see partial results, or does the query layer detect the inconsistency and fall back to the primary? Capture the exact sequence of alerts, retries, and manual interventions that follow. Over several runs, patterns emerge—maybe the system recovers gracefully from compute failures but falls over when a cache gets cold, or maybe a single slow downstream call cascades into thread pool exhaustion.
Only after you have run these scenarios and documented the recovery paths should you consider the system ready for acceptance. If a particular failure mode leaves the team scrambling with no clear rollback or failover procedure, that is not a sign-off condition—it is a gap to close before production. Signing off without this evidence means you are betting that failures will happen on someone else's watch, and that someone will have to learn the system's breaking points the hard way.
FAQ
Look beyond just frequency and power. Check the transducer's uniformity across the entire tank, because hot spots can cause inconsistent cleaning or even damage. Also examine the ability to control energy density per surface area, temperature stability, and the range of frequency sweeping or modulation. A system that only runs at a fixed frequency may not handle varied particle sizes or delicate features well.
Insist on seeing damage threshold data for materials similar to yours, not just generic charts. Ask for a controlled trial where they run your actual parts or coupons through the system and then perform surface analysis (e.g., SEM, AFM) to check for micro-cracking, erosion, or lifted films. A reputable vendor will also offer adjustable power and duty cycle settings to stay well within the safe operating window.
Material compatibility is often overlooked until failures happen. The vendor should demonstrate that the chemistry, temperature, and megasonic energy won't attack the substrate, coatings, or embedded structures. For example, some polymers and thin metal films degrade under prolonged cavitation. Ask for compatibility test reports and evidence of handling mixed-material assemblies without cross-contamination.
Megasonic cleaning behaves differently on polished optics, semiconductor wafers, ceramic substrates, and micro-machined metals. A vendor with direct experience in your industry understands the failure modes and knows how to tune parameters to avoid creating new defects. They should be able to reference specific case studies or customer references without hiding behind generic marketing claims.
You need more than a certificate of compliance. Ask for detailed process qualification protocols, including control limits, monitoring methods, and data logging capabilities. A good vendor will provide IQ/OQ/PQ support and help you establish in-line monitoring for bath life, particle counts, and acoustic output. If they can't show a clear traceability path from process parameters to part quality, keep looking.
Don't just check footprint and power requirements. Evaluate communication interfaces (SECS/GEM, Ethernet/IP, or simple dry contacts), chemical handling and exhaust needs, and whether the tank design fits your current automation. Request a site survey and ask about required facility modifications. A vendor who offers modular or customizable tank sizes and rack designs will save you from costly retrofits later.
Ask about mean time between failures for transducers and generators, not just the warranty period. Find out if they stock critical spare parts locally, what the typical response time is, and whether they offer remote diagnostics. Also clarify who is responsible for transducer replacement and recalibration—some vendors hide those costs in the fine print. A strong service network matters more than a low upfront price in high-volume precision manufacturing.
Watch out for vendors who push a single standard configuration without asking about your specific part geometry and contamination challenges. If they avoid providing customer references or can't explain how their system maintains acoustic uniformity over time, that's a warning sign. Also be suspicious of claims that one system works for every material and particle size without parameter adjustments—megasonic cleaning is highly application-dependent.
Conclusion
Before sending RFQs, take time to identify the exact contaminant you are fighting—is it submicron particulate, organic residue, or a thin film left from previous processing? This matters more than any vendor's claimed frequency or power density. Two systems can list identical transducer frequencies, yet their cavitation behavior may differ sharply across a wafer or precision component. Ask for acoustic mapping data, not just a spec sheet. The cleaning chemistry and megasonic energy must also be tuned as a pair; a solvent that works in immersion may be nearly useless under megasonic agitation, or it may generate excessive radicals that attack delicate surfaces. So shortlist vendors who are willing to run chemistry-energy trials on your actual parts.
Tank geometry is another factor that quietly decides particle removal rate. Even a well-designed transducer can be undermined by a tank shape that creates standing waves or dead zones near the part fixture. Ask vendors to show removal efficiency at multiple locations inside the tank, not just the center. Cleanroom references from precision manufacturing sites carry far more weight than polished marketing claims. Request case studies involving similar substrates, feature sizes, and contamination types. Finally, before signing off, run a controlled damage study using real devices or patterned test wafers. Look for micro-cracking, pattern collapse, or residue redeposition. Only after both cleaning performance and damage risk are verified should the system be accepted.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/