Why Choosing the Right China Water Jet Sewer Machine Supplier Matters for Your Project
2026-11-16
When a sewer line fails, every hour of downtime quietly drains your budget. Many contractors discover too late that the machine they bought was never engineered for real field conditions—only for a spec sheet. Choosing the right China water jet sewer machine supplier is not just about getting a lower price. It is about matching pump performance, hose reach, and after-sales support to the demands of your project. Working with a focused manufacturer like AMJET changes that equation: you gain direct access to technical insight, faster spare parts, and machines that hold pressure when the job gets difficult. Before you compare quotes, it is worth understanding why supplier selection often decides whether a sewer cleaning project finishes on time or turns into a costly lesson.
The Low Bid Often Becomes the Most Expensive Machine on the Job
The bid price is rarely the number that decides a machine’s true cost. Once a low-bid machine starts missing cycles, eating filters, or waiting on a parts truck that never seems to arrive before Friday, the savings disappear. A loader that sits idle for a week costs more in schedule damage than the discount ever returned.
Some costs are easy to ignore because they don’t appear on the invoice. Fuel burn that runs high, hydraulic leaks that delay fine grading, and resale value that drops hard all belong to the machine. The cheap option often earns its reputation on job sites where the crew can’t afford another breakdown.
None of this means the highest quote is automatically the right choice. It means the low bid should be read as a risk, not a win. The most expensive machine on the job is the one that fails when it’s needed most.
A Factory Floor Tells You More Than a Glossy Spec Sheet
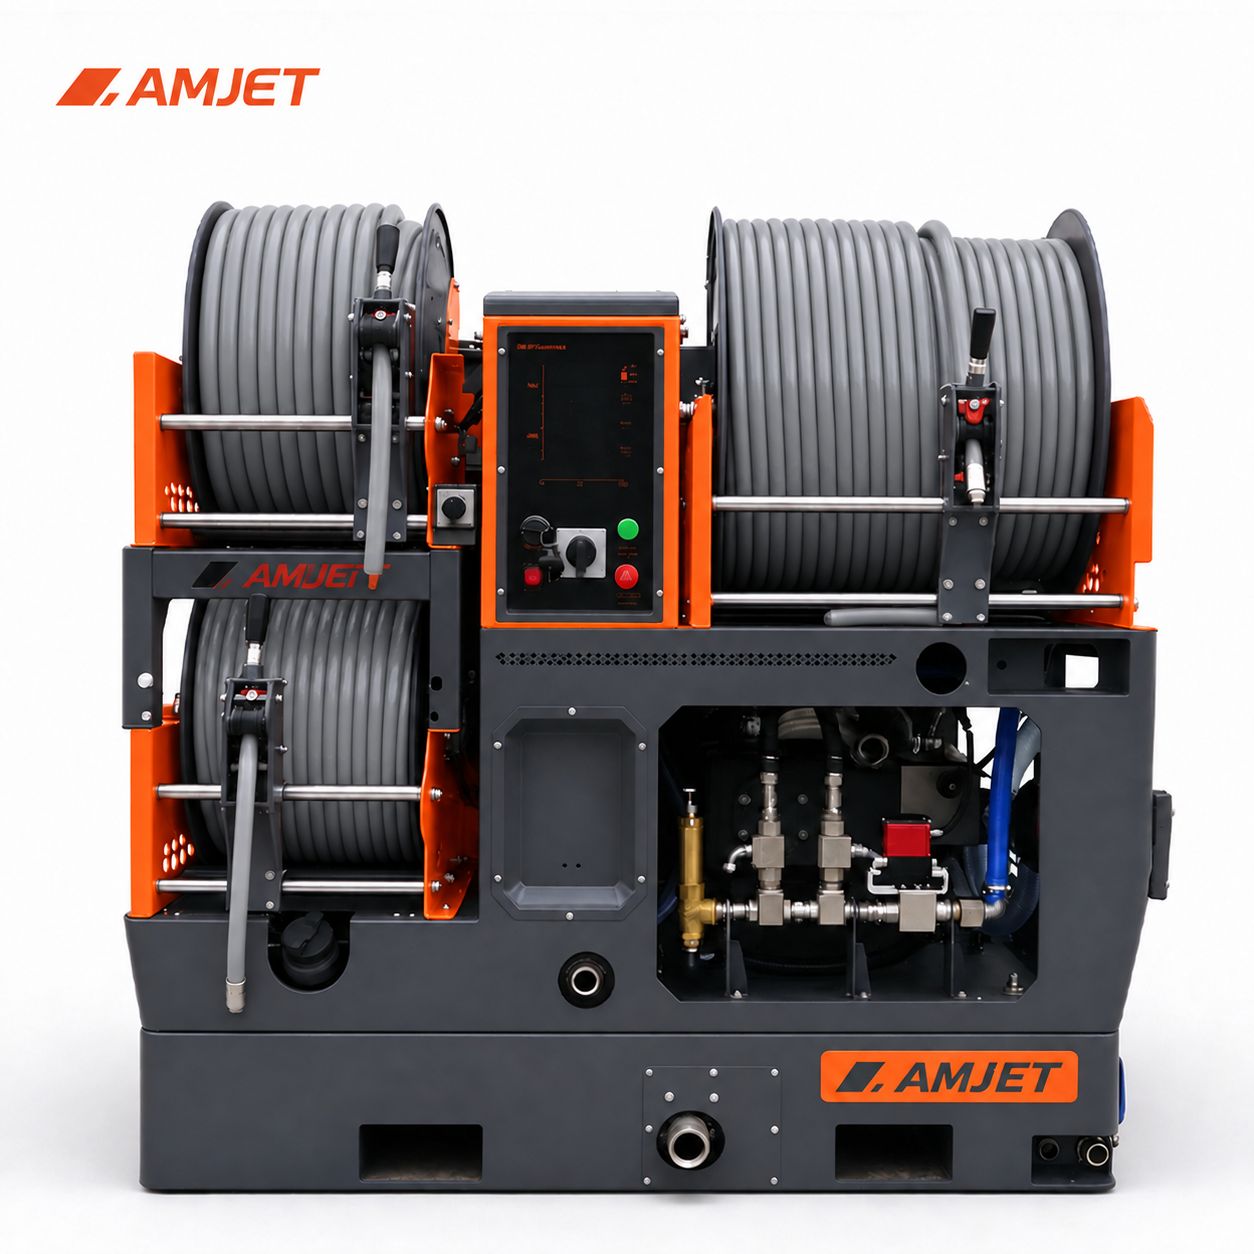
Walk through any production facility and you will see the real story in the way materials move, how workers adjust to small hiccups, and where unfinished units collect dust. A polished brochure can list tolerances and throughput numbers, but it rarely captures the smell of cutting fluid, the pace of a shift change, or the quiet pride of someone loading a fixture for the ten-thousandth time. Those details matter because they reveal whether a process is genuinely under control or merely photographed at its best angle.
On the floor, claims about lean manufacturing or zero-defect culture either hold up under casual observation or fall apart within an hour. You notice whether tooling is organized or scattered, whether people pause to help a neighbor without being asked, and whether quality checks happen at the point of work or get rushed near the shipping dock. None of that fits neatly into a spec sheet, yet it shapes the product far more than any polished surface finish.
Buyers and engineers often focus on measurable outputs, but the most useful audits happen when nobody is expecting one. A short walk past raw stock, assembly benches, and outbound packaging can expose bottlenecks, rework loops, and the small improvisations that never make it into official documentation. When you see those patterns with your own eyes, the gap between a vendor's promise and their actual capability becomes impossible to ignore.
Pump Pressure Claims Mean Nothing Without the Right Nozzle and Hose Match
A pressure figure stamped on a pump rarely reflects what happens at the nozzle. That number is usually recorded under a specific flow rate with a specific orifice size, and once the machine is assembled with a hose that is longer, narrower, or fitted with restrictive couplers, the working pressure can drop before water ever leaves the tip. In other words, the pump is only one part of a hydraulic circuit, and its rating says little about cleaning force until the rest of that circuit is known.
Nozzle selection changes everything. An orifice that is too large lets water escape too freely, so the pump cannot build its claimed pressure and impact drops off. An orifice that is too small pushes the system toward a pressure spike, which wears seals and valves faster while producing a thin, aggressive jet that may not clean evenly. The hose matters just as much. Every extra foot of hose and every narrow quick-connect fitting creates friction loss, quietly erasing a portion of the pump's advertised PSI before you squeeze the trigger.
The number worth paying attention to is the pressure at the spray gun inlet with the full hose length connected and the intended nozzle installed. That reading depends on matching the pump's flow output to the right orifice and a hose diameter that can carry that flow without excessive restriction. When those pieces align, the pump's claim becomes something you can actually measure at the surface. Until then, a big PSI sticker is just a laboratory condition, not a cleaning result.
After Delivery, the Supplier's Response Time Becomes the Real Warranty
The moment a product ships, many buyers assume the hardest part is over. In practice, what follows the delivery often matters more than the delivery itself. A warranty on paper means little if the supplier takes days or weeks to reply when something goes wrong. The real promise is not the document tucked inside the box but the speed and clarity of the first response after a problem is reported.
Fast response times change how faults are experienced. A delayed answer turns a minor issue into a major frustration, while a quick reply can keep a production line moving or a customer calm. Suppliers who treat post-delivery communication as a core service rather than an afterthought build a different kind of trust. They know that the first 24 hours after a claim often decide whether a relationship survives the next order.
This is why response time deserves the same attention as defect rates or delivery dates. Measuring how long a supplier takes to acknowledge a warranty claim, provide a diagnosis, or propose a replacement is not a bureaucratic exercise. It reveals whether the company sees warranty as a cost to be minimized or a chance to prove reliability when it actually counts.
Custom Orders Stall When the Factory Doesn't Understand Local Pipe Conditions
A batch of custom flanges sits in a warehouse while the client waits for photos of a corroded pipeline that was never on any spec sheet. The factory keeps asking for the outer diameter and wall thickness, but the real problem is the uneven pressure curve and the way joints shift when the ground settles. Until those local quirks are measured and discussed, the order stays frozen.
Some buyers try to bridge the gap by sending videos of the trench, old fittings, or a hand-drawn sketch of the bypass. That helps more than a data table because it shows where standard dimensions stop working. When the production team still treats the order like another stock item, revisions pile up, delivery windows close, and a project that should have moved forward waits on a single misunderstood detail.
Spare Parts Shouldn't Require a Six-Week Container Wait Every Time
When a hydraulic seal fails on a Tuesday, the real cost is never just the replacement part. It is the idle excavator, the crew standing around, and a project timeline that starts sliding before anyone has even approved the purchase order. Yet too many equipment owners still accept that a small rubber or steel component has to sit inside a shipping container for six weeks because the regional warehouse only stocks fast-moving SKUs. That math rarely holds up once downtime is counted in hours rather than days.
Keeping critical spares closer to the equipment does not mean duplicating an entire catalog in every market. It means identifying the parts that stop work most often and positioning those items in smaller forward-stock locations, then backing them with air freight only for genuine exceptions. A six-week sea freight window should be the last resort for slow-moving castings, not the default answer for a coupling or sensor that can shut down a whole machine.
Customers remember the week they waited far longer than they remember the invoice line for freight. A spare parts operation that plans around actual failure patterns, seasonal demand, and equipment age can usually deliver in days without inflating inventory. The container is not the problem; treating every part as if it belongs on a slow boat is.
FAQ
This equipment runs at thousands of PSI and often gets used daily in tough conditions. A supplier with weak quality control can deliver a machine that fails at a coupling or pump seal, and that downtime eats into your project schedule. The right supplier understands operating pressure, flow rate, and component durability, not just how to assemble a frame around a pump.
Ask how they test each unit before shipping. Look for documented pressure tests, leak checks, and run-time verification rather than a simple visual inspection. A supplier that keeps records for each machine and shares those reports openly is usually more dependable than one that only promises quality.
Talk to them about nozzle size, hose diameter, flow requirements, and pressure loss. A knowledgeable supplier will ask about your pipe sizes, blockage types, and typical job length before recommending a configuration. If they only quote a machine without asking about your application, that is a warning sign.
Low cost often shows up later as thinner frames, weaker hoses, or pumps that cannot maintain rated pressure over time. You may save money upfront but lose it through frequent repairs, missed deadlines, and frustrated crews. Long-term cost per operating hour matters more than the purchase price alone.
Very important for specialized work. You might need a specific hose reel length, a trailer or skid mount, extra water tank capacity, or controls set up for a particular operator position. A supplier that can adjust these details without treating every change as a major engineering project gives you equipment that fits your crews and site conditions.
Clarify warranty coverage, which parts are included, and how quickly they can ship replacements. Also ask for troubleshooting support after delivery, whether by email, video call, or phone. A supplier that stays responsive after payment is the one that will keep your machine working over the long haul.
Ask for references from buyers in similar industries and contact them directly. Request photos or videos of recent builds, and look for details like weld quality, hose routing, and component brands. If possible, ask for a live factory walk-through or independent inspection before the machine leaves the workshop.
The dependable supplier treats your machine as a working tool, not just a sale. They stock common wear parts, maintain clear documentation, and keep their engineering team involved when you need changes. Over time, that reduces delays and keeps your sewer cleaning work moving without constant equipment headaches.
Conclusion
A sewer cleaning machine looks straightforward on paper, but the real cost shows up once it reaches the job site. The lowest bid rarely stays low: undersized components, mismatched pumps, and generic nozzles turn routine blockages into repeated call-outs, damaged pipes, and idle crews. Visiting the factory floor often reveals what a glossy spec sheet cannot—whether weld quality, assembly tolerances, and testing procedures are consistent, or whether the line is racing to push out containers. Pump pressure numbers also mean little on their own. A machine only performs when the pump curve, hose diameter, and nozzle orifice are matched to the actual pipe diameters and debris load. If suppliers treat these as interchangeable parts, the claimed bar rating becomes a marketing line rather than a cleaning result.
Delivery is not the finish line. The supplier’s response after the invoice is paid becomes the real warranty, and a time-zone-delayed answer or a missing service manual can stall a municipal crew for days. Custom orders fail when the factory assumes every sewer network behaves like a clean test bench; local pipe materials, root intrusion, silt levels, and access points have to shape the build, not just the paint color. Spare parts should be stocked or air-freighted in days, not buried in a six-week container schedule. Choosing the right supplier means looking past the quote and evaluating engineering honesty, onsite support, and parts availability before the first hose is ever unrolled.
Contact Us
Contact Person: Mike
Email: [email protected]
Tel/WhatsApp: +86 19545555505
Website: https://www.amjeting.com/